In today’s fast-paced industrial environment, the efficiency of operations is paramount for staying competitive. A key component in enhancing productivity is the use of conveyors and conveyor systems. These systems not only streamline the movement of goods but also significantly reduce the manual labour needed in various processes. However, selecting the right conveyor for your operation can be a daunting task due to the plethora of options available.
Understanding the capabilities, limitations and suitability of different conveyor types is crucial. This guide aims to elucidate the critical factors to consider when selecting the right conveyors for your business, enabling you to make informed decisions that align with your operational needs.
Conveyors are vital components in various industries, streamlining the transportation of goods and materials. They enhance efficiency by reducing manual handling and improving workflow. However, challenges can arise, such as ensuring that objects properly follow the conveyor’s movement. For those troubleshooting these issues, a helpful resource can be found here: https://forums.developer.nvidia.com/t/conveyor-belt-moving-but-object-not-following-help-needed/310765. Understanding conveyor systems is essential for seamless operations.
Importance of Conveyor Systems
Conveyor systems are integral to many industries, including manufacturing, logistics, and distribution. These systems facilitate the seamless movement of goods, contributing to increased efficiency and reduced lead times. Implementing the right conveyor can drastically improve your workflow and can lead to significant cost savings in the long run.
The choice of conveyor system affects everything from the speed and efficiency of your operations to the quality control processes in place. By investing time in understanding the various types of conveyors available and their applications, you can elevate your operational efficiency to new heights.
Types of Conveyors
When considering conveyor systems, it’s essential to recognise the various types available, each serving distinct purposes and industries. Here are some of the most common types of conveyors:
Belt Conveyors
Belt conveyors are among the most widely used types in industry. They consist of a continuous loop of material—typically rubber, plastic, or metal—that runs over pulleys. Ideal for transporting bulk materials or lighter goods over long distances, belt conveyors are particularly versatile. They are suitable for horizontal or inclined applications and can easily accommodate various load sizes.
Roller Conveyors
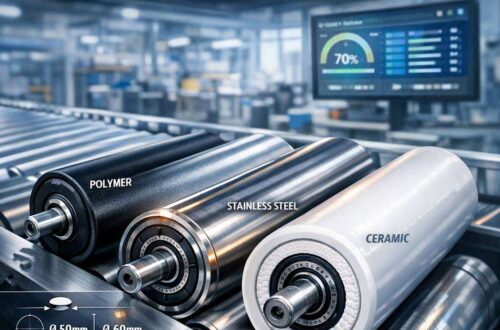
Roller conveyors are another popular choice. They utilise a series of rollers to move goods, either through the application of gravity or powered means. Gravity roller conveyors are passive and best suited for handling items manually, while powered roller conveyors offer more control and speed, making them ideal for automated systems.
Chain Conveyors
Chain conveyors are perfect for transporting heavy and bulky items. They feature a chain that runs through a track, offering superior strength and durability compared to other types. In applications where heavier loads are common, chain conveyors excel due to their ability to handle extreme weights without faltering.
Conveyors are integral to modern manufacturing and logistics, streamlining the transportation of goods and materials. They enhance efficiency, reduce labor costs, and minimize handling time. Whether for moving heavy items in a warehouse or transporting delicate products in a packaging line, conveyors come in various types to suit diverse needs. With reliable solutions available, businesses can improve productivity by investing in the right conveyor systems. Learn more about effective conveyor options at https://conveyorrollers.co.uk.
Screw Conveyors
Used primarily for bulk materials, screw conveyors are designed to move material along a tubular casing. They are particularly effective for handling granular, powdered, or liquid materials. Their enclosed structure makes them an excellent choice for applications needing protection from contamination or environmental damage.
Frequently Asked Questions about Conveyors
What are conveyors?
Conveyors are mechanical devices used to transport materials or products from one location to another within a facility. They can be used in various industries, including manufacturing, agriculture, and logistics, ensuring efficient and seamless movement of goods.
How do conveyors work?
Conveyors operate using a belt or other means to move items along a path. The basic components include the conveyor frame, drive mechanism (such as motors), pulleys, and the carrying medium (like belts or rollers) that moves the materials.
What types of conveyors are available?
There are several types of conveyors available, including:
- Belt Conveyors: Utilises continuously moving belts.
- Roller Conveyors: Uses rollers for product movement.
- Chain Conveyors: Employs chains to carry heavy loads.
- Screw Conveyors: Moves bulk material through a rotating screw within a tube.
- Flexible Conveyors: Allows for adaptable layouts in packaging and shipping operations.
What industries commonly use conveyors?
Conveyors find applications across various sectors such as:
- Manufacturing
- Food processing
- Warehousing and distribution
- Mining
- PharmaceuticalsThese industries rely on conveyor systems for increased efficiency and productivity.
What factors should be considered when selecting a conveyor system?
When selecting a conveyor system, consider the following factors:
- Material Type: Weight, size, shape.
- Distance Needed to Cover: Overall length requirements.
- Environment Conditions: Temperature variations or exposure to chemicals.
- Production Volume: Volume capacity necessary for operations.
- Integration Needs: Compatibility with existing equipment.
How can I maintain my conveyor system effectively?
Maintaining your conveyor system involves regular inspections and preventive maintenance such as:
- Checking belt tensioning and alignment
- Regularly greasing bearings
- Inspecting for wear on components
- Cleaning debris from belts or rollers
- Monitoring motor performance
Regular maintenance helps prolong the life of your equipment.
Can conveyors be customized?
Yes! Many manufacturers offer customisation options based on specific industry needs such as size adjustments, speed modifications, or unique configurations tailored to your operational processes.
Are there safety considerations with using conveyors?
Absolutely! Safety measures must be implemented when using conveyors which may include:
- Installing safety guards over dangerous moving parts
- Providing training for workers
- Adhering to weight limits
4 . Providing emergency stop functions
Prioritizing safety reduces risks associated with operating these systems.
Considerations When Choosing Conveyors
Selecting the appropriate conveyor system requires careful consideration of various factors. Here are some key elements to keep in mind when making your decision:
Weight and Type of Material
Understanding the weight and type of material you intend to transport is vital. Certain conveyors are designed for light products, while others can handle heavy machinery or large quantities of materials. Always consult with your supplier to ensure compatibility with your specific application.
Speed and Efficiency
The speed at which your conveyor system operates greatly impacts the overall productivity of your facility. Evaluate the required throughput to ensure the conveyor you select meets your operational needs. Many systems allow you to adjust speed settings for flexibility, helping to optimise workflow.
Installation Space
The layout of your facility also plays a significant role in your choice of a conveyor system. Consider the space you have available and whether you’ll need a fixed or movable system. It is vital to carefully plan the conveyor’s path, keeping in mind not just the available space, but also the flow of materials throughout your operations.
Maintenance and Durability
Maintenance requirements and the durability of your conveyor system are crucial operational factors. Some systems require regular upkeep, while others are nearly maintenance-free. Invest in a system that suits your operational capacity and maintenance budget. Paying attention to warranties and the availability of replacement parts can aid in prolonging the conveyor’s life.
Customisation and Integration
Finally, the ability to customise and integrate your conveyor system with existing equipment should not be overlooked. Custom conveyor solutions that account for your specific needs can greatly enhance the efficiency of your operations. Whether you need special features like sensors, controls, or product alignment, working with a knowledgeable supplier can ensure that all aspects are thoroughly considered.
Implementing a cohesive conveyor system can yield significant benefits by improving the efficiency and reliability of your operations. Take the time to evaluate your options and invest in the right conveyor solution to propel your business forward. By doing so, you position your operations to meet current demands and adapt more effectively to the future.